Tissue Rewinding Machine Factory Secrets to High-Speed Converting
2026-09-21
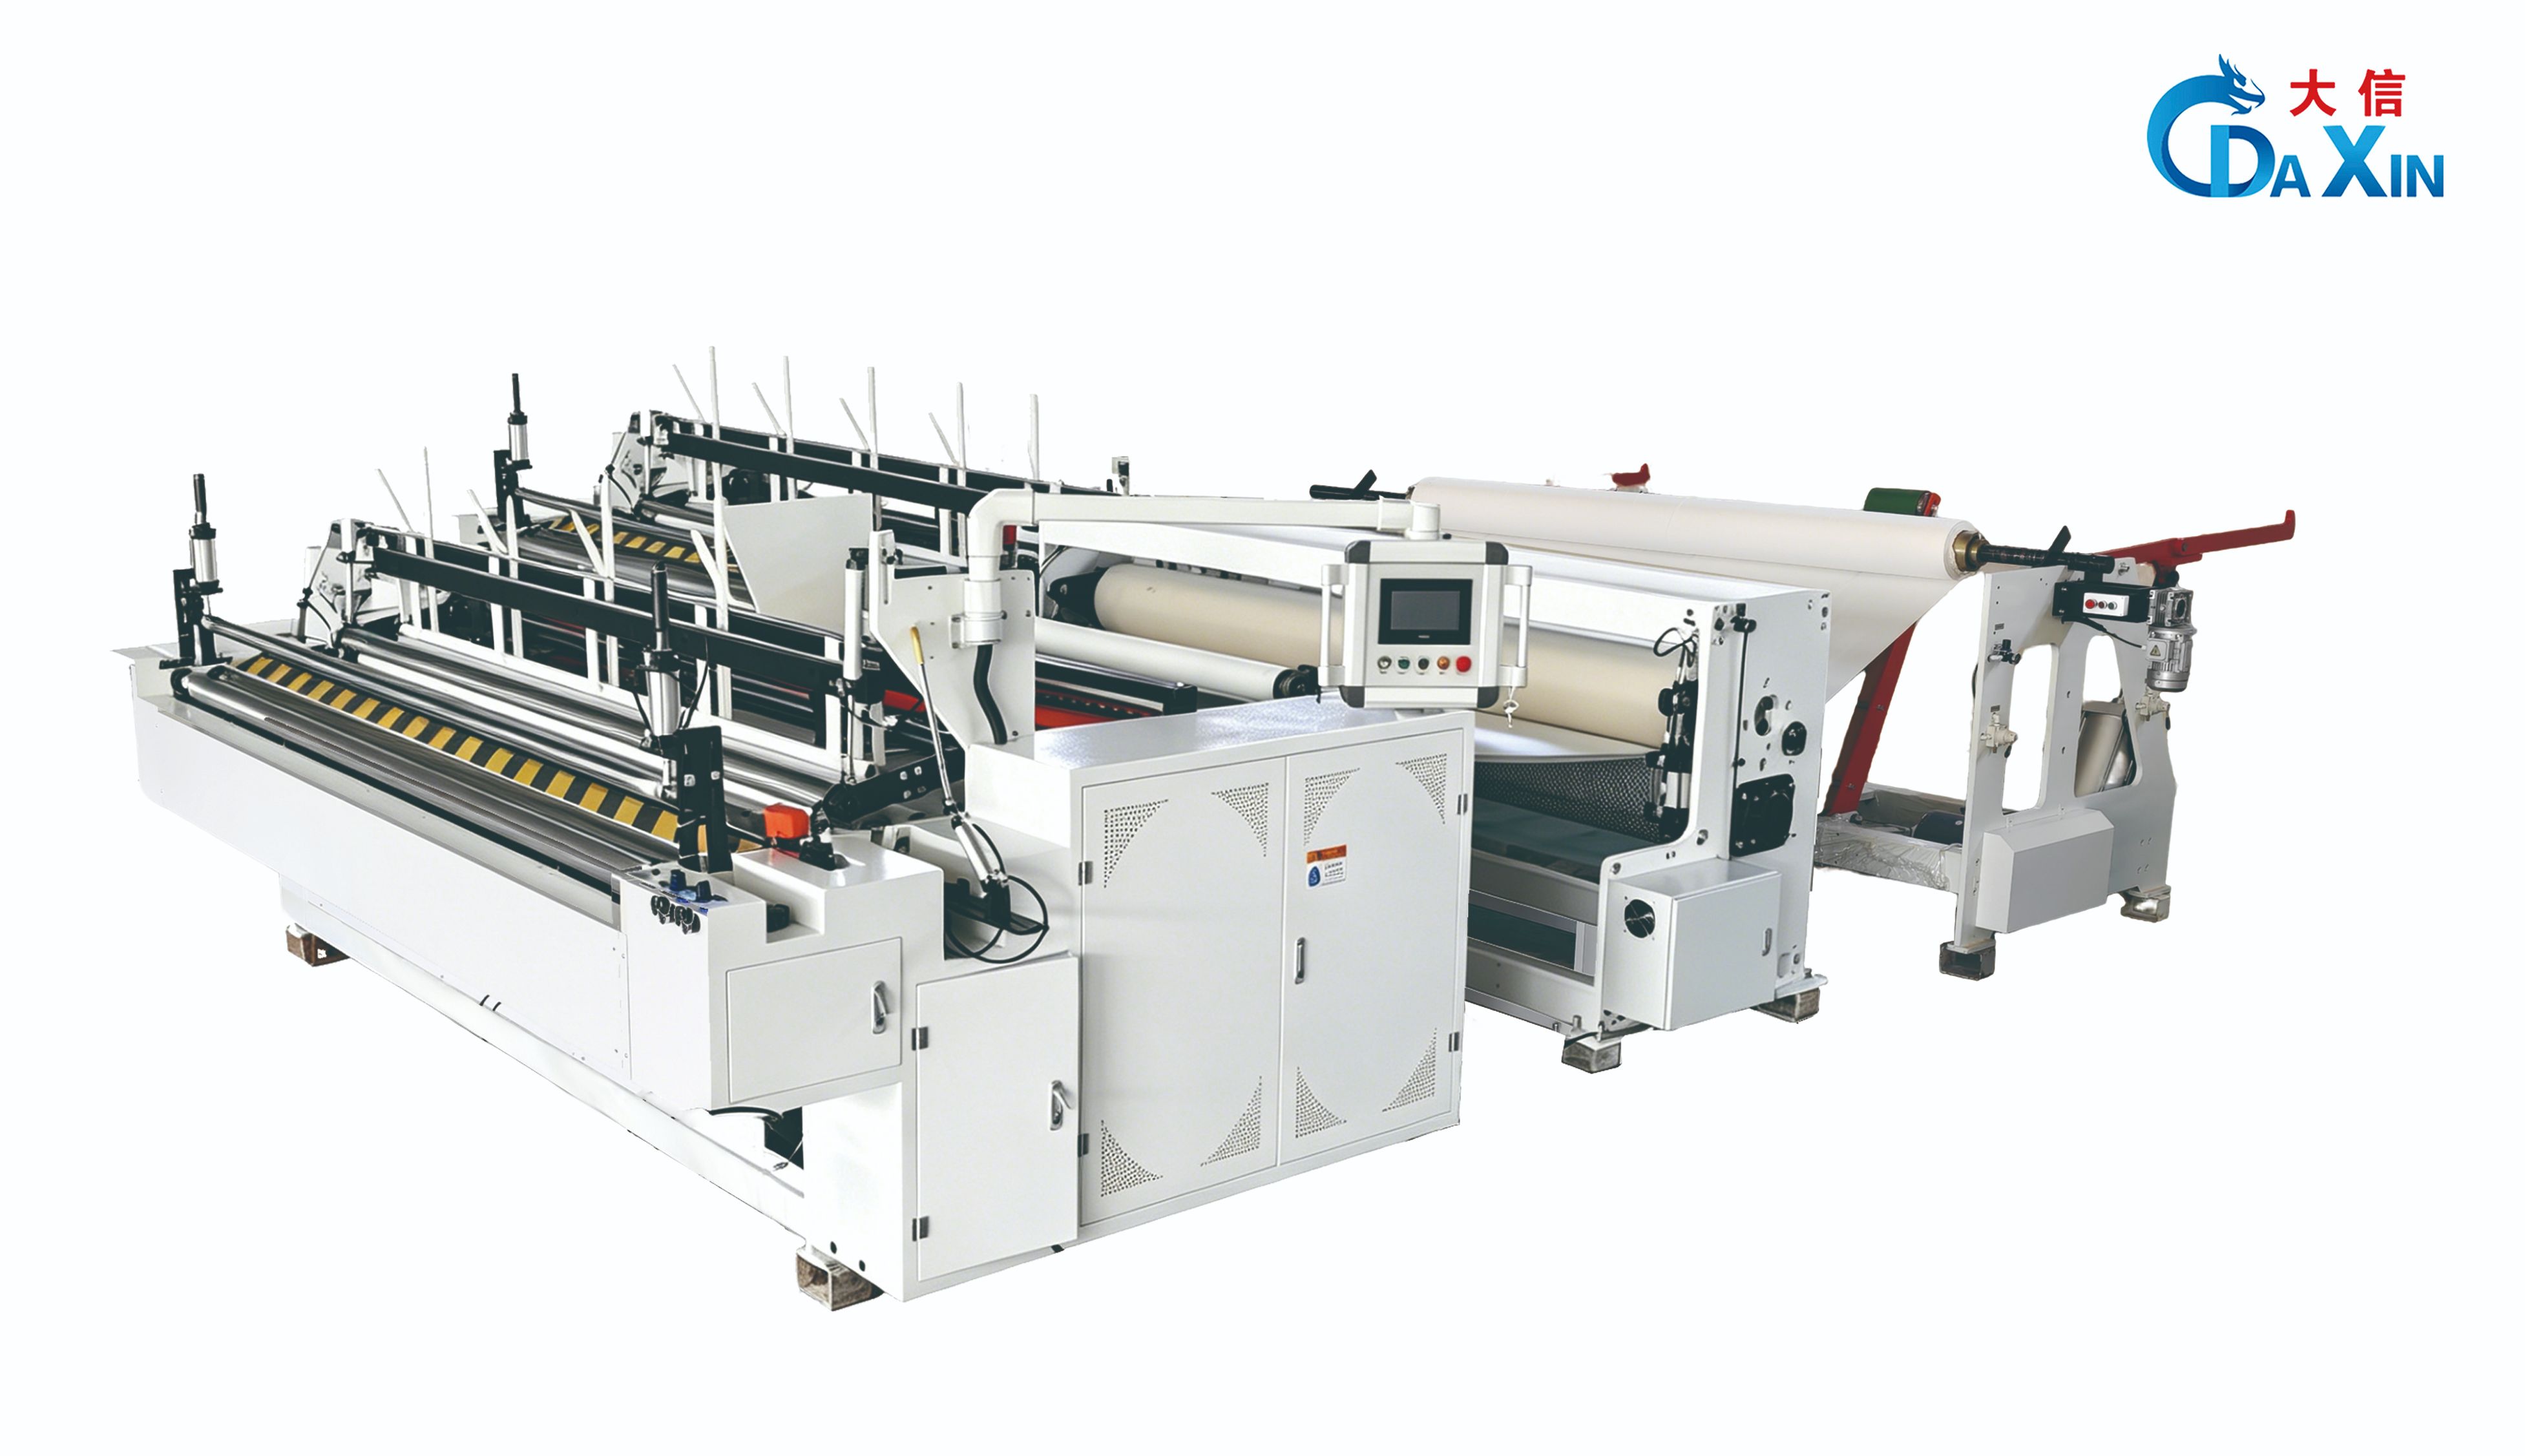
Walk into any tissue converting plant and you’ll hear the same complaint: the rewinder is the bottleneck. Yet most factories keep buying machines that look identical on paper. After spending time on the floor at DAXIN, I realized high-speed converting isn’t about a bigger motor—it’s about how the rewinding drums, tension control, and splice systems work together without forcing operators to slow down. Here’s what actually separates a line that crawls from one that sustains 600 meters per minute without turning rolls into confetti.
What Floor Managers Actually Tweak When a Tissue Line Hits 600 Meters a Minute
At 600 meters a minute, the floor manager stops watching the line and starts listening to it. The first thing they adjust is tension on the unwind stand—too tight and the sheet snaps at the creping blade, too loose and you get wrinkles that follow the sheet all the way to the reel. Most managers keep a small notebook with tension readings for each parent roll, because a ten-millimeter drift can turn a clean run into a dust storm in under two minutes.
Next comes the yankee coating. As speed climbs, the coating spray pattern has to shift from a soft mist to a fine, angled jet, otherwise the blade chatters and the sheet picks up those tiny hard particles that end up as pinholes in the finished towel. Experienced floor managers will also bump the creping blade angle half a degree and lower the blade pressure just enough to keep the bulk high without losing adhesion—it's a feel thing, not a number you'll find in the manual.
Finally, they watch the converting section. At this line speed, even a small air gap in the tail threading can cause the sheet to fold over on itself and jam the stacking belt. So managers tend to stand near the folder and make live tweaks to the vacuum pull-off rolls and the slitter blades—opening the gap a hair, then closing it, listening for that clean zipping sound that tells you the sheet is cutting true. Every adjustment is small, but together they're what keep a 600-meter tissue line from turning into a confetti machine.
The Tension Zone Nobody Puts on the Spec Sheet
Every product carries a set of numbers that promise compatibility, speed, or capacity. But between those columns of figures sits a less flattering space: the small daily frictions that only show up after the first week. Heat buildup at a particular angle, a connector that works but needs a third hand, a noise floor that changes character under load. None of these make it into the comparison table, yet they shape how the thing actually feels.
That gap is the tension zone. It is not a defect in the traditional sense. It is the accumulated mismatch between how a device was measured and how it gets used. Engineers might call it edge-case ergonomics or unmodeled interaction. Users just call it the reason they switch brands. The absence of a label for this zone does not make it less real; it simply means the burden of discovering it falls entirely on the person holding the product.
Good design does not eliminate the tension zone; it acknowledges it. Teams that spend time in real kitchens, workshops, or server closets tend to produce things that feel more forgiving, not because the numbers improved but because the hidden friction was reduced. That is rarely printed on a box, but it is the difference between something you tolerate and something you reach for without thinking.
Why a Dull Blade Can Quietly Kill Your Rewinding Output
A blade that has lost its edge doesn't just cut poorly—it tears, frays, and drags. On a rewinder, this shows up as fuzzy edges, inconsistent roll diameters, and sporadic web breaks. Each of those defects forces the operator to slow the line, trim away spoiled material, or stop for a blade change. Over a shift, that quiet drag compounds into lost output that never appears on a downtime report.
The real cost hides in the details. A dull blade demands more cutting pressure, which accelerates wear on anvils, bearings, and tension controls. The resulting micro-stops and speed reductions are rarely logged as blade-related, so the problem lingers. Sharpening on a fixed schedule instead of waiting for visible failure keeps the rewind running at nameplate speed and turns blade maintenance from a hidden bottleneck into a predictable, low-cost routine.
How to Read Wrinkles Like a Rewinder Technician
Wrinkles tell you more than just the age of a roll. They map out exactly where tension went wrong, which roller lost its grip, and how the web fought back against misalignment. A rewinder technician learns to read these lines the way a tracker reads footprints—each crease has a direction, a cause, and a story about the machine's condition at that exact moment.
Start by looking at the angle of the wrinkle. Diagonal lines drifting toward one edge usually mean the web wandered off center or a roller wasn't parallel to its neighbor. Short, tight crinkles near the core suggest the initial winding tension was too high for the material's stiffness. Long, wavy undulations across the full width point to uneven nip pressure or a bowed roller that should have been straightened weeks ago.
Once you can identify these patterns on sight, you stop guessing and start fixing. You'll know whether to adjust the lay-on roller, tweak the differential shaft, or simply clean a sticky idler. The roll itself becomes your diagnostic report—no sensors needed, just a trained eye and the willingness to trace every line back to its source.
Overnight Runs: The Calibration Checks That Prevent 3 a.m. Shutdowns
The plant's overnight runs are more than just a routine procedure—they're the first line of defense against the kind of sudden shutdowns that send maintenance crews scrambling at three in the morning. By running calibration checks during the quiet hours when load demand dips, operators can catch sensor drift, valve timing issues, and flow meter discrepancies that would otherwise go unnoticed until they snowball into a full-scale fault.
These checks aren't about finding problems that already exist; they're about predicting the ones that will. A slightly offset pressure transducer might not trigger an alarm at 2 p.m., but at 3 a.m., when ambient temperatures drop and condensate builds, that same error can cross a threshold and trip a safety interlock. The overnight window gives engineers a controlled environment to simulate low-load conditions and verify that every feedback loop responds within tolerance.
Teams that skip these runs often learn the hard way: the cheapest fix is the one you make before the system forces your hand. A thirty-minute calibration sequence at midnight is far less costly than a six-hour emergency restart, not to mention the knock-on effects for downstream processes that rely on steady output. It's not about being paranoid—it's about respecting the physics of aging instruments and the reality of thermal cycling.
From Operator Memory to Repeatable High-Speed Setups
A lot of shops still carry setup knowledge in people's heads. One operator might know the exact order to loosen clamps, the feel of a dial indicator, or the odd shim thickness that makes a fixture repeat. That works until that person calls in sick or retires—and every new setup becomes a slow, uncertain process. Turning that private memory into something the whole team can use is the first real step toward repeatable high-speed changeovers.
The shift usually starts with capturing what the best operator actually does, not what the manual says. Short videos, annotated photos, and simple checklists pinned to the machine beat formal documentation because they mirror real sequences. Then you hard-code those steps into the equipment: pinned locations, quick-release clamps, preset tool offsets, and color-coded gauges. When a step can't be forgotten or done out of order, speed follows automatically.
The result is a setup process that no longer depends on one person's memory. A new or cross-trained operator can follow the visual cues and hit the same positions within minutes instead of hours. Setup time becomes stable and predictable, which means more spindle time and less standing around. Over time, those small captured details compound into a serious competitive edge—not from working harder, but from not having to relearn the job every run.
FAQ
Usually the bottleneck isn't the rewinder itself but how well the finished log density and core centering are controlled. Factories that hold diameter within a millimeter and keep the core centered can push the downstream saw and wrapper much harder without jams or tear-outs.
For 15 to 18 gsm stock you need closed-loop tension with load cells near the winding drum, plus tapered tension that drops as the roll builds. Relying on open-loop dancer position alone invites breaks and soft edges once the line crosses about 500 meters per minute.
They use differential winding shafts and keep the pressure between winding drums and the building roll constant through the cycle. The best lines profile that nip pressure against the measured roll diameter instead of using a fixed pneumatic setting.
Perforation blade material and holder rigidity matter more than people admit. Carbide or ceramic blades with a rigid cross-machine beam let you hold a clean perforation at high cycles, while cheap steel flexes and produces ragged cuts that force frequent stops.
If the embosser runs even slightly off-phase with the rewinder, the pattern smashes the sheet and you lose caliper. Top factories monitor phase drift continuously and correct within a fraction of a millimeter, which keeps bulk loss under two or three percent.
Caliper, moisture, and wound-in tension maps from the jumbo roll tell you whether you can run flat out or need to derate. A quick check of the roll hardness profile with a Schmidt hammer is cheap and prevents most web breaks that get blamed on the rewinder.
They place the tail exactly on a treated strip and use temperature-controlled glue that sets fast but stays flexible. Purging old adhesive and checking nozzle alignment every shift matters more than increasing the glue volume.
Operators who do a 90-second pre-flight on core glue, perforation phase, and tension settings before threading almost never have first-log failures. Plants that skip that routine lose more time on restarts than they ever save by hurrying.
Conclusion
When a tissue line climbs to 600 meters a minute, floor managers aren't relying on guesswork. They're dialing in the subtle variables that spec sheets ignore: the exact pressure profile on the rider roll, the micro-adjustments to unwind brake response, and how the core glue pattern interacts with high-speed vibration. One of the least discussed culprits in output loss is blade dullness—it doesn't just leave ragged edges, it forces the rewinder to compensate with extra tension, which in turn amplifies wrinkles and triggers splice breaks. Experienced technicians learn to read wrinkles as a live diagnostic: short diagonal creases near the core point to acceleration imbalance, while long horizontal waves suggest a misaligned spreader bar. Overnight runs live or die by calibration checks done before the shift ends—bearing temperature checks, nip load verification, and a quick laser alignment on the unwind stand can mean the difference between a clean 3 a.m. handoff and a shutdown that erases the week's efficiency gains.
The real factory secret isn't a single trick; it's converting operator memory into repeatable high-speed setups. Instead of relying on a veteran's intuition, top plants now capture every parameter from a successful 600 m/min run—tension ramp curves, air pressure on the lay-on arm, even the exact blade angle after sharpening—and store them as digital recipes. That way, the tension zone nobody puts on the spec sheet becomes a controlled variable rather than a mystery. The result is a rewinding line that doesn't just hit high speed occasionally, but does it shift after shift, with fewer wrinkles, fewer blade changes, and far fewer 3 a.m. phone calls.
Contact Us
Contact Person: Sam Xie
Email: [email protected]
Tel/WhatsApp: 86-18938538530
Website: https://www.daxin321.com/