OEM Rapid Transfer Port Essentials for Cleanroom Operations
2026-09-28
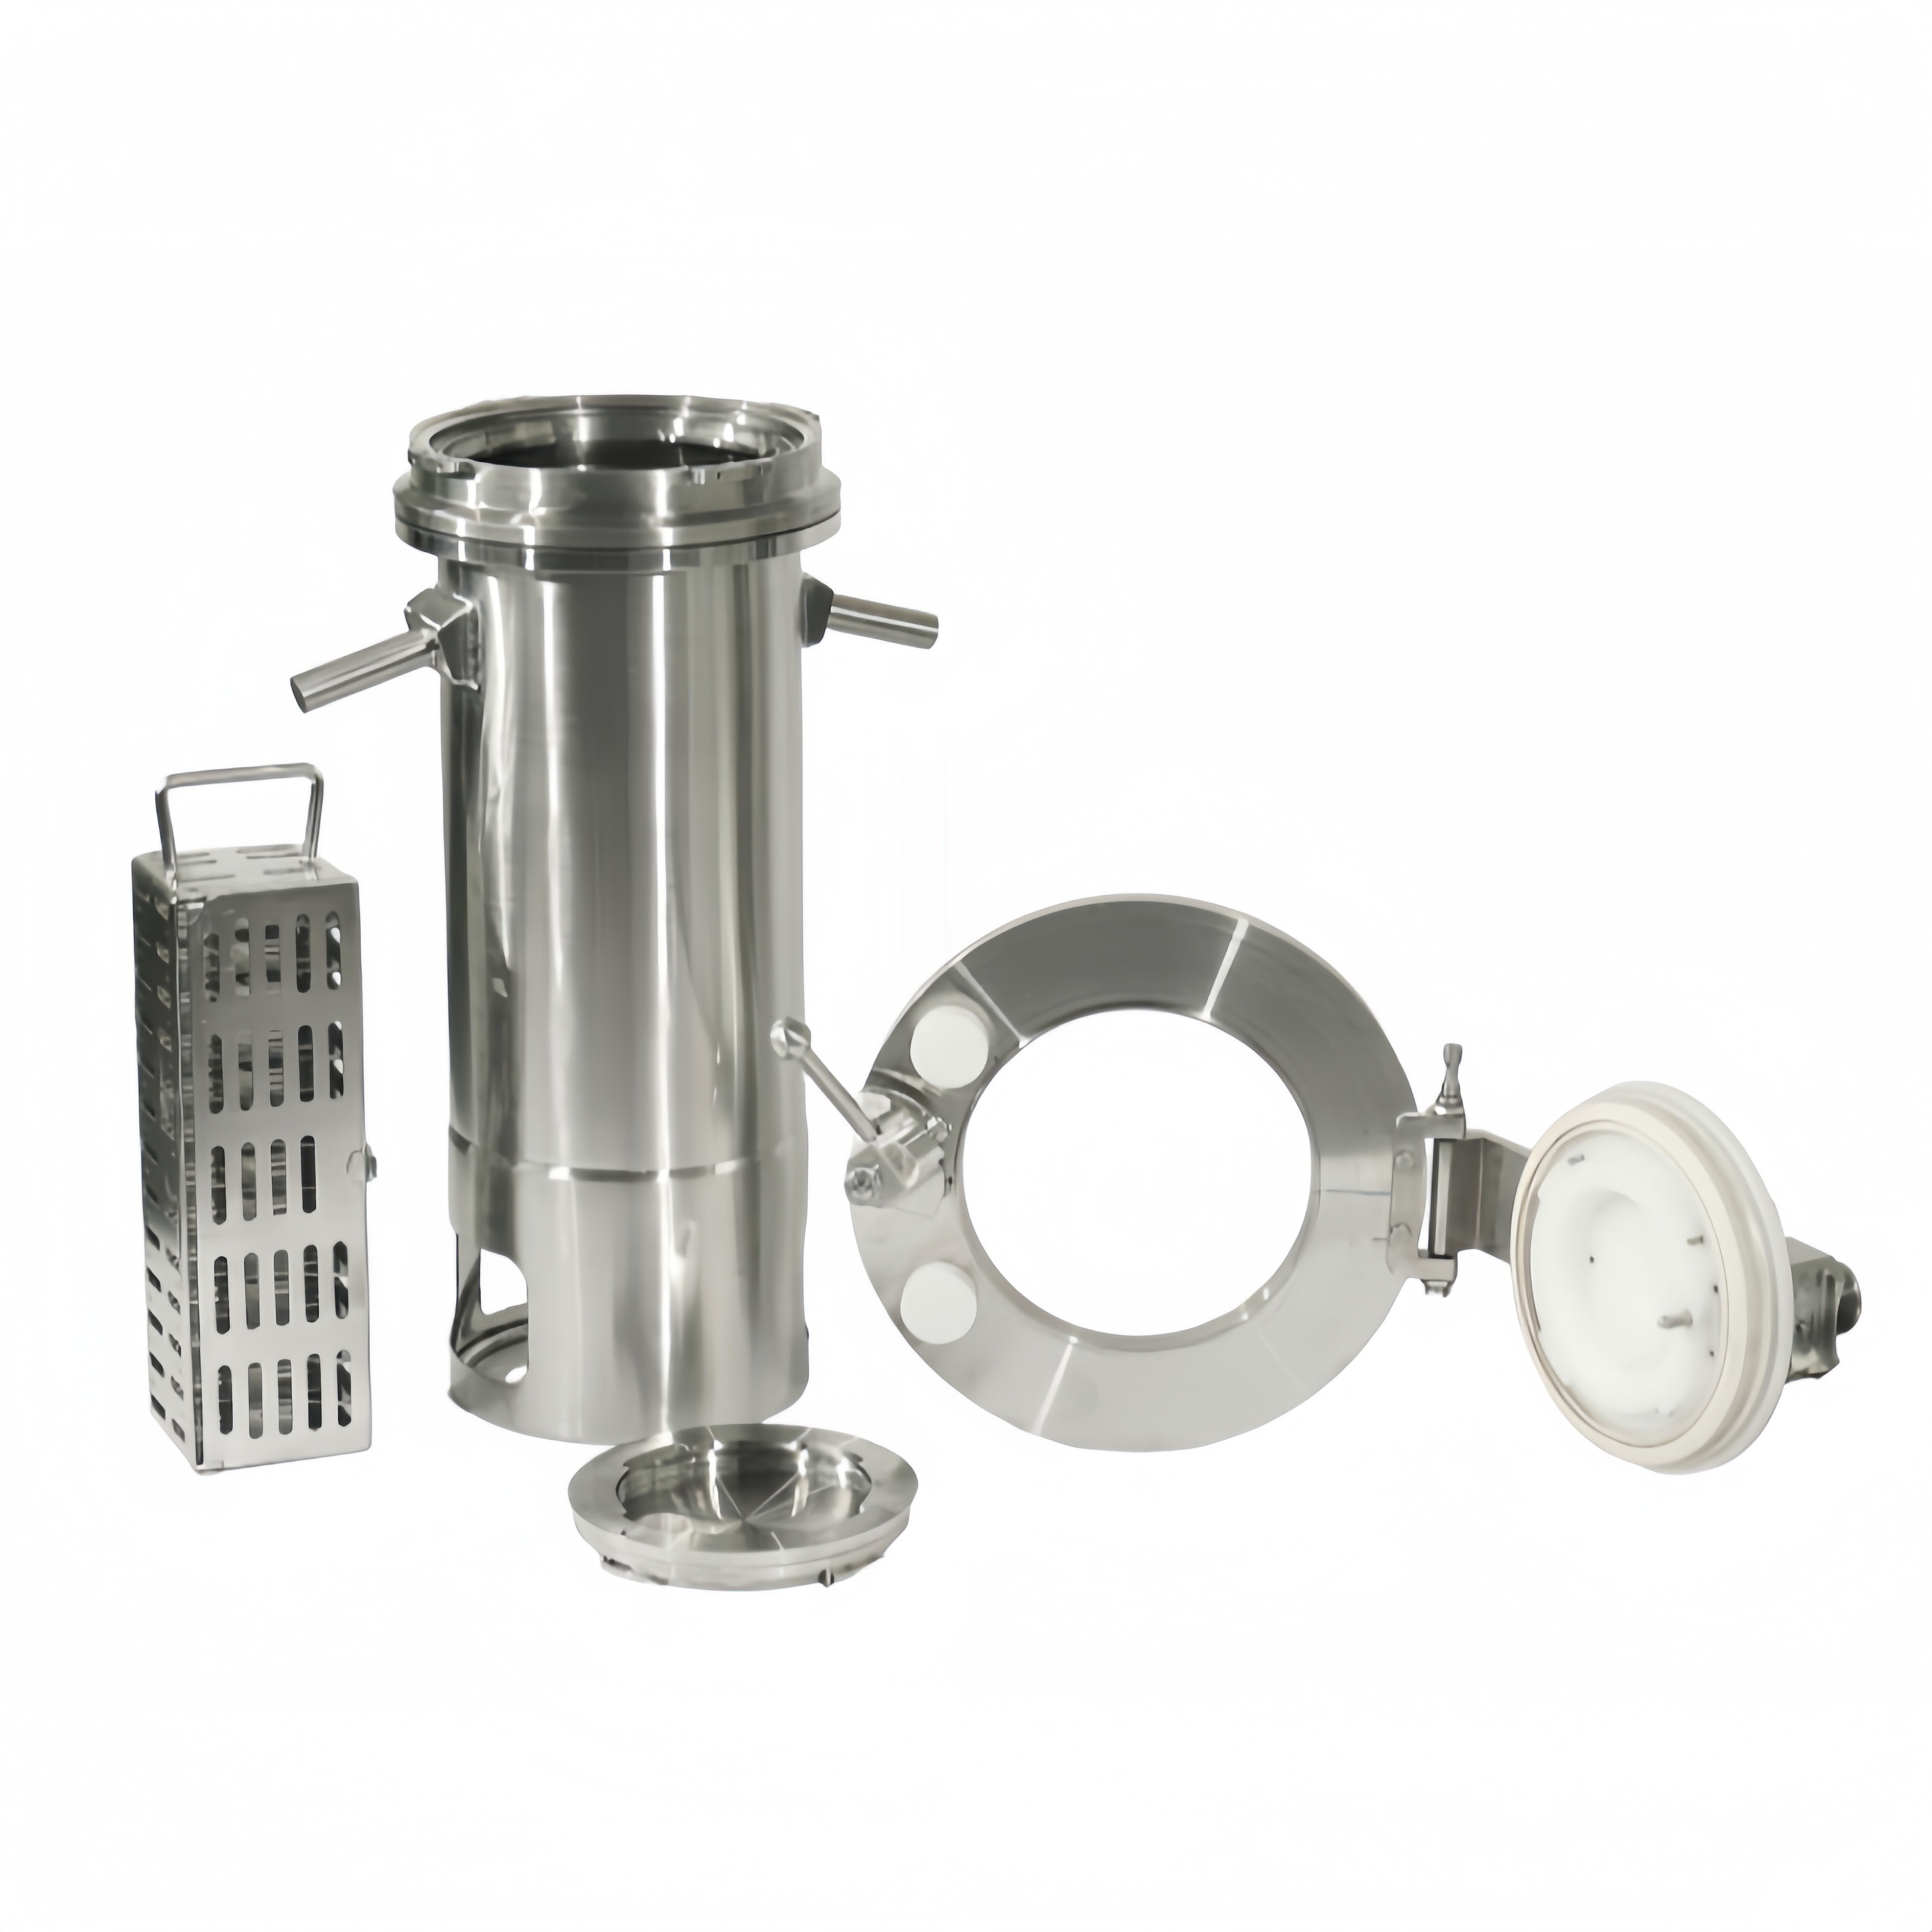
When contamination risks rise, most cleanroom teams focus on gowning, HEPA filters, and airflow—yet the transfer ports connecting critical zones often go unexamined. That's a costly blind spot. OEM rapid transfer ports aren't interchangeable commodities; their design, sealing integrity, and material compatibility directly affect sterility assurance and operational uptime. At AVM, we've seen how the right port choice prevents breaches and simplifies validation. This guide breaks down the essentials you need before specifying or upgrading your system.
Port Placement That Doesn't Fight Your Workflow
Most laptops force you to adapt to their port layout, but this one was designed around how you actually work. Instead of cramming every connector onto one side, the ports are separated by function and reach. Charging sits at the back left, so the cable never crosses your mouse hand. High-speed USB and video output live on the right, where a typical right-handed user expects them. This isn't about symmetry—it's about not interrupting your flow.
What really matters is the small stuff. The headphone jack is up front, not buried behind other cables. The SD card slot is recessed just enough to avoid accidental ejections but still easy to find by touch. Even the USB-C ports are spaced so that two chunky adapters can sit side by side without fighting for room. No more unplugging one thing to plug in another.
After a week of use, the placement starts to feel invisible, which is the whole point. You stop thinking about where things go because your hand already knows. That's a rare thing in a laptop, and it comes from studying how people actually sit, reach, and move—not from arranging ports to look good in a product photo.
Gasket Checks Most Teams Skip Until It's Too Late
Most mechanics glance at a gasket for cracks or tears, then bolt everything back together. That's the easy miss. The real killer is compression set—when the material loses its spring and just lies there flat. A gasket can look brand new on the outside and still be dead inside. Next time you pull a flange apart, run a fingernail across the surface. If it doesn't bounce back or leaves a permanent trench, it was already leaking before you touched it.
Torque sequences get skipped because they feel slow. Someone grabs an impact gun, runs the bolts in a circle, and calls it good. That uneven squeeze shoves the gasket sideways—maybe a fraction of a millimeter, enough to thin one edge permanently. Later, under heat cycles, that thin spot becomes the path of least resistance. By the time you see the weep, the gasket is already extruded into the bolt holes. And no one remembers who did the last install.
Reusing a metal or graphite gasket "just this once" is a gamble most shops take without thinking. The surface looks fine, the color's normal, so it goes back in. But those materials work by conforming to micro-scratches on the flange face. Once they've been crushed once, they can't conform again. If the flange is aluminum or has any pitting, a reused gasket will seal for a week, maybe a month, then start seeping exactly where you can't see it until the puddle forms. Cheaper to bin it than chase the leak later.
Why Your Transfer Port Leaks Even When It Looks Sealed
A transfer port can look completely tight to the naked eye yet still let fluid or gas escape. The reason usually comes down to surface finish, not just clamping force. Even a freshly machined face has tiny peaks and valleys. When two surfaces meet, those irregularities leave micro-channels that can open under pressure. If the mating faces are not lapped or if the seal material has hardened over time, the escape path is already there before you ever notice a drop.
Temperature swings make the problem worse by changing clearances inside the assembly. Metals expand at different rates, and elastomer seals take a compression set after enough heat cycles. Once an O-ring loses its ability to rebound, it no longer fills the groove the way it did when new. That is why a port can hold fine on the bench and then seep after one full run cycle.
The only reliable way to catch this is not by eye but by testing under real conditions. A quick bubble check or holding pressure for a few seconds often misses slow migration through a microscopic gap. Swap in a known-good seal, check flatness with a straightedge and feeler gauge, and then retest at the pressure and temperature the system actually sees. If the leak disappears, the old part was the silent culprit all along.
Cleanroom Airflow Around the Port: The Invisible Variable
Even the smallest interruption in a cleanroom’s airflow can quietly compromise sterility, and few elements are as overlooked as the area immediately surrounding a transfer port. When a port is opened or closed, the careful balance of unidirectional air is disturbed: eddies form, pressure differentials shift, and particles that had been safely swept away can linger near the opening. The result is not always visible, but it can be measured in microbial counts and product failures weeks later.
Understanding this invisible variable requires moving beyond generic airflow models. The geometry of the port, the frequency of use, and the position of return vents all shape how air behaves at this boundary. In many facilities, a perfectly designed cleanroom is undone by a single poorly integrated port that creates a standing vortex, drawing contaminated air from the operator’s side into the aseptic zone. Even low-profile designs can cause subtle backflow if the pressure cascade across the wall is not actively maintained.
Practical solutions often focus on local airflow visualization and real-time pressure monitoring. Smoke studies reveal the truth that theoretical calculations miss: a port that appears flush and sealed may still leak air during operation. Adjusting the supply air angle, adding a small extraction grille near the port, or simply repositioning the operator’s workflow can restore the intended sweeping effect. The key is treating the port not as an isolated barrier, but as a dynamic participant in the cleanroom’s air management strategy.
Training Operators to Read the Port, Not Just the Manual
A manual can tell an operator what a gauge should read, but it cannot teach the smell of low tide on a wind shift, the way a crane's groan changes when a load is off-center, or the subtle back-eddy that signals a barge is about to swing wide. Reading the port means learning to trust peripheral vision and gut feel—the accumulated pattern recognition that separates a competent button-pusher from someone who keeps a berth safe when the weather turns.
We drill this by pulling trainees out of the classroom and onto the quay during live operations. Instead of reciting checklist steps, they call out what they see before asking what the book says. A deckhand might notice that a line is taut in a way that doesn't match the tension meter, or a forklift driver spots how a stack of containers leans two degrees more than yesterday's log recorded. That discrepancy is the port talking.
The goal isn't to discard manuals but to make them subordinate to the working environment. When an operator can stand at the rail, read the water, the wind, and the hull's response all at once, they stop reacting to alarms and start preventing them. That's the difference between following instructions and knowing the job.
Upgrading an OEM Port Without Voiding the Warranty
Most owners assume any change to the OBD port immediately kills the warranty, but that fear is often overblown. The trick is to stick with plug-and-play upgrades that don't require cutting, splicing, or soldering into the factory harness. A simple pass-through adapter or a diagnostic dongle that clicks into the existing port leaves the original wiring untouched, which is exactly what dealerships look for when deciding whether a modification caused a problem.
Look for hardware that carries the right certifications for your region—CE, FCC, or an OEM-approved badge. Avoid anything that promises to “unlock” hidden features by rewriting the ECU or altering voltage levels. Instead, choose extensions that preserve every original pin and function, so you can unplug the upgrade in thirty seconds before a service visit and the port looks bone stock.
Keep the original dust cap, any zip ties you removed, and the factory mounting clips in a labeled bag. If a warranty claim ever comes up, being able to show that the port itself was never physically altered—and that your upgrade was fully reversible—goes a long way. Many manufacturers’ warranty guides explicitly allow temporary accessories, and a clearly documented, reversible install puts you on solid ground without needing a lawyer.
FAQ
Instead of just providing a static barrier opening, an OEM RTP is engineered to integrate directly with existing isolator or RABS flange geometry. It uses a double-door alpha/beta principle, so the beta canister's door becomes the interface surface—meaning you're not just moving materials, you're maintaining a validated seal across two environments without breaking containment. The OEM part means the port dimensions, locking mechanism, and door materials are all matched to your specific equipment, not retrofitted.
It rarely comes down to just bag volume. You look at the largest component you'll pass—lyophilized product trays, 200L bags, tooling—plus the handling ergonomics on the cleanroom side. If your transfer requires a 350mm or 420mm diameter beta flange, many stock models won't cover that. Custom OEM lets you specify door swing direction, interlock timing, and even gasket material for vapor-phase hydrogen peroxide compatibility without adding an adapter ring that can trap contamination.
316L stainless steel for structural parts is pretty standard, but the gaskets and seals are where it gets tricky. You need EPDM or silicone that holds up to repeated decontamination cycles with vaporized hydrogen peroxide or chlorine dioxide. Some OEMs offer perfluoroelastomer (FFKM) door seals if the suite sees strong oxidizers or solvents. The beta canister door often uses a transparent polycarbonate or borosilicate glass window, but that material has to be chemically compatible with your wipe-down agents, not just the drug product.
Often yes, if the wall opening can be enlarged to fit a standard flange frame. The challenge is sealing the frame to the panel on both the dirty and clean sides with no crevices. You don't want a flange gasket that's just glued—mechanical compression with a cleanroom-grade silicone or closed-cell foam is better. For an OEM solution, the supplier should provide a template or come on site to measure the actual opening before cutting. That avoids the "field adjustment" that often ruins a good panel.
At minimum, ask for an installation qualification (IQ) package that includes dimensional drawings, torque specs for flange bolts, and a material certificate for every wetted and non-wetted component. If the RTP is going into a GMP grade A/B environment, you'll also need data showing the dual-door seal maintains a positive pressure differential during dynamic air flow—not just a static leak test. Some vendors only provide a pressure decay test at 250 Pa; you really want a smoke study or microsphere challenge result that matches your actual cleanroom pressure cascade.
Replacement cycles vary with decontamination frequency, but a good rule is to inspect seals every six months and replace at the first sign of cracking, permanent compression set, or if the beta canister requires increasing force to latch. A failing seal often shows up as a slow drop in chamber pressure during a negative pressure hold test, or visible vapors escaping during a VHP cycle. Don't wait for a particle count excursion—proactive replacement is far cheaper than a batch investigation.
That sticking often comes from polymer degradation of the door gasket or buildup of hydrogen peroxide residues on the alignment pins. If the pins are stainless steel but the bushing is plastic, slight thermal expansion differences can cause galling. To prevent it, use a PTFE or ceramic bushing, apply a minimal amount of approved dry lubricant to the latch mechanism only, and include a brief post-cycle purge in your VHP routine that fully dries the door interface. Never use standard silicone spray—it just traps more oxidizer next to the elastomer.
The real control is procedural, not just hardware. Each beta canister should be dedicated to a product or at least a product family, and the canister door should be removed and cleaned in a validated parts washer between campaigns. The alpha port on the isolator side should be wiped with the same disinfectant used for the glove ports, but you must include contact time. Some sites also use a disposable liner inside the beta canister for high-risk products, which turns the RTP into a "bag-in/bag-out" system without sacrificing the rapid transfer speed.
Conclusion
In cleanroom operations, the rapid transfer port is rarely the center of attention until a contamination event forces it there. The first decision that shapes daily performance is placement. A port installed at the edge of a workflow or at an awkward height creates a quiet bottleneck—operators lean, stretch, or double-handle materials, and every unnecessary motion works against the controlled environment. Equally invisible until failure is the gasket. Teams often skip routine tactile checks, assuming a visual once-over is enough. But micro-tears, compression set, and residue buildup can leave a port looking sealed while leaking at the interface. Pressure decay testing or a simple gloved-finger sweep along the seal often reveals what a quick glance misses.
Leaks themselves are rarely dramatic; they are pressure differentials that develop slowly, influenced by cleanroom airflow around the port. Supply air patterns, adjacent equipment, or even a partially opened door can create local turbulence that draws unfiltered air across the seal. That is why training has to move beyond the manual. Operators need to read the port itself—feel for resistance changes, listen for the subtle click of a fully seated flange, and recognize when the interlock catches early. And when an OEM port needs upgrading, the path is not necessarily a full replacement. Many improvements—adding a validated gasket material, repositioning the mounting frame within the existing cutout, or installing an airflow deflection shield—can be done without voiding the warranty if discussed with the manufacturer beforehand. The goal is to keep the port as a true barrier, not a ritualized part of the routine.
Contact Us
Contact Person: Ananda
Email: [email protected]
Tel/WhatsApp: 8619016718200
Website: https://www.wzaomi.com