Aluminum Intake Manifold Maker for High-Performance Engines
2026-09-16
Every extra horsepower in a high-performance engine starts with how well it breathes. Aluminum intake manifolds are a proven way to sharpen throttle response and reduce weight, but only when the casting, port alignment, and surface finish are done right. DDR has focused on exactly that: building manifolds that hold up under aggressive tuning without the usual compromises. Here’s what to look for in a maker, and why the details matter before you bolt one on.
The Metallurgy Behind Our Aluminum Choices
Aluminum's appeal often gets reduced to a single number—weight—but the real story lives in the alloys themselves. Most people don't realize that pure aluminum is practically useless for structural work. It's soft, gummy under cutting tools, and prone to galling. What transforms it is the deliberate introduction of elements like magnesium, silicon, copper, and zinc, each one shifting the metal's behavior in subtle ways. A 6061 frame and a 7075 bracket might look identical on a spec sheet's weight column, yet their fatigue lives and yield strengths diverge by a factor of two or more. The metallurgy isn't a footnote; it's the entire reason one part survives a decade of vibration while another cracks in a season.
Heat treatment adds another layer of stubborn complexity. Precipitate hardening, for instance, relies on a nanoscale dance: quench the alloy fast enough to trap solute atoms in a supersaturated solid solution, then age it at a low temperature to coax out tiny clusters that pin dislocations. Get the aging window wrong—leave it in the oven twenty minutes too long—and those clusters coarsen into useless chunks. The result is a part that bends like taffy instead of springing back. This sensitivity is why aerospace shops and bicycle builders obsess over exact oven temperatures and water-quench delays. It's not mysticism; it's just that the margin between perfect and mediocre lives in a few hundred degrees and a few seconds.
Grain structure is the third leg of the stool, and it's the one designers rarely see on a data sheet. Extruded aluminum, rolled plate, and forged billets each carry a distinct texture from how the metal flowed during forming. A tensile test pulled along the extrusion direction can report a beautiful number, while the same bar tested across the grain fails at 60 percent of that value. Anodizing behavior shifts too: grain boundaries near the surface can etch at different rates, leaving a mottled finish that no amount of polishing fixes. Smart material selection means asking where the load path runs, not just how big the load is. Otherwise you end up with a beautifully machined component that splits along a plane nobody thought to check.
Port Matching Secrets for Flawless Airflow
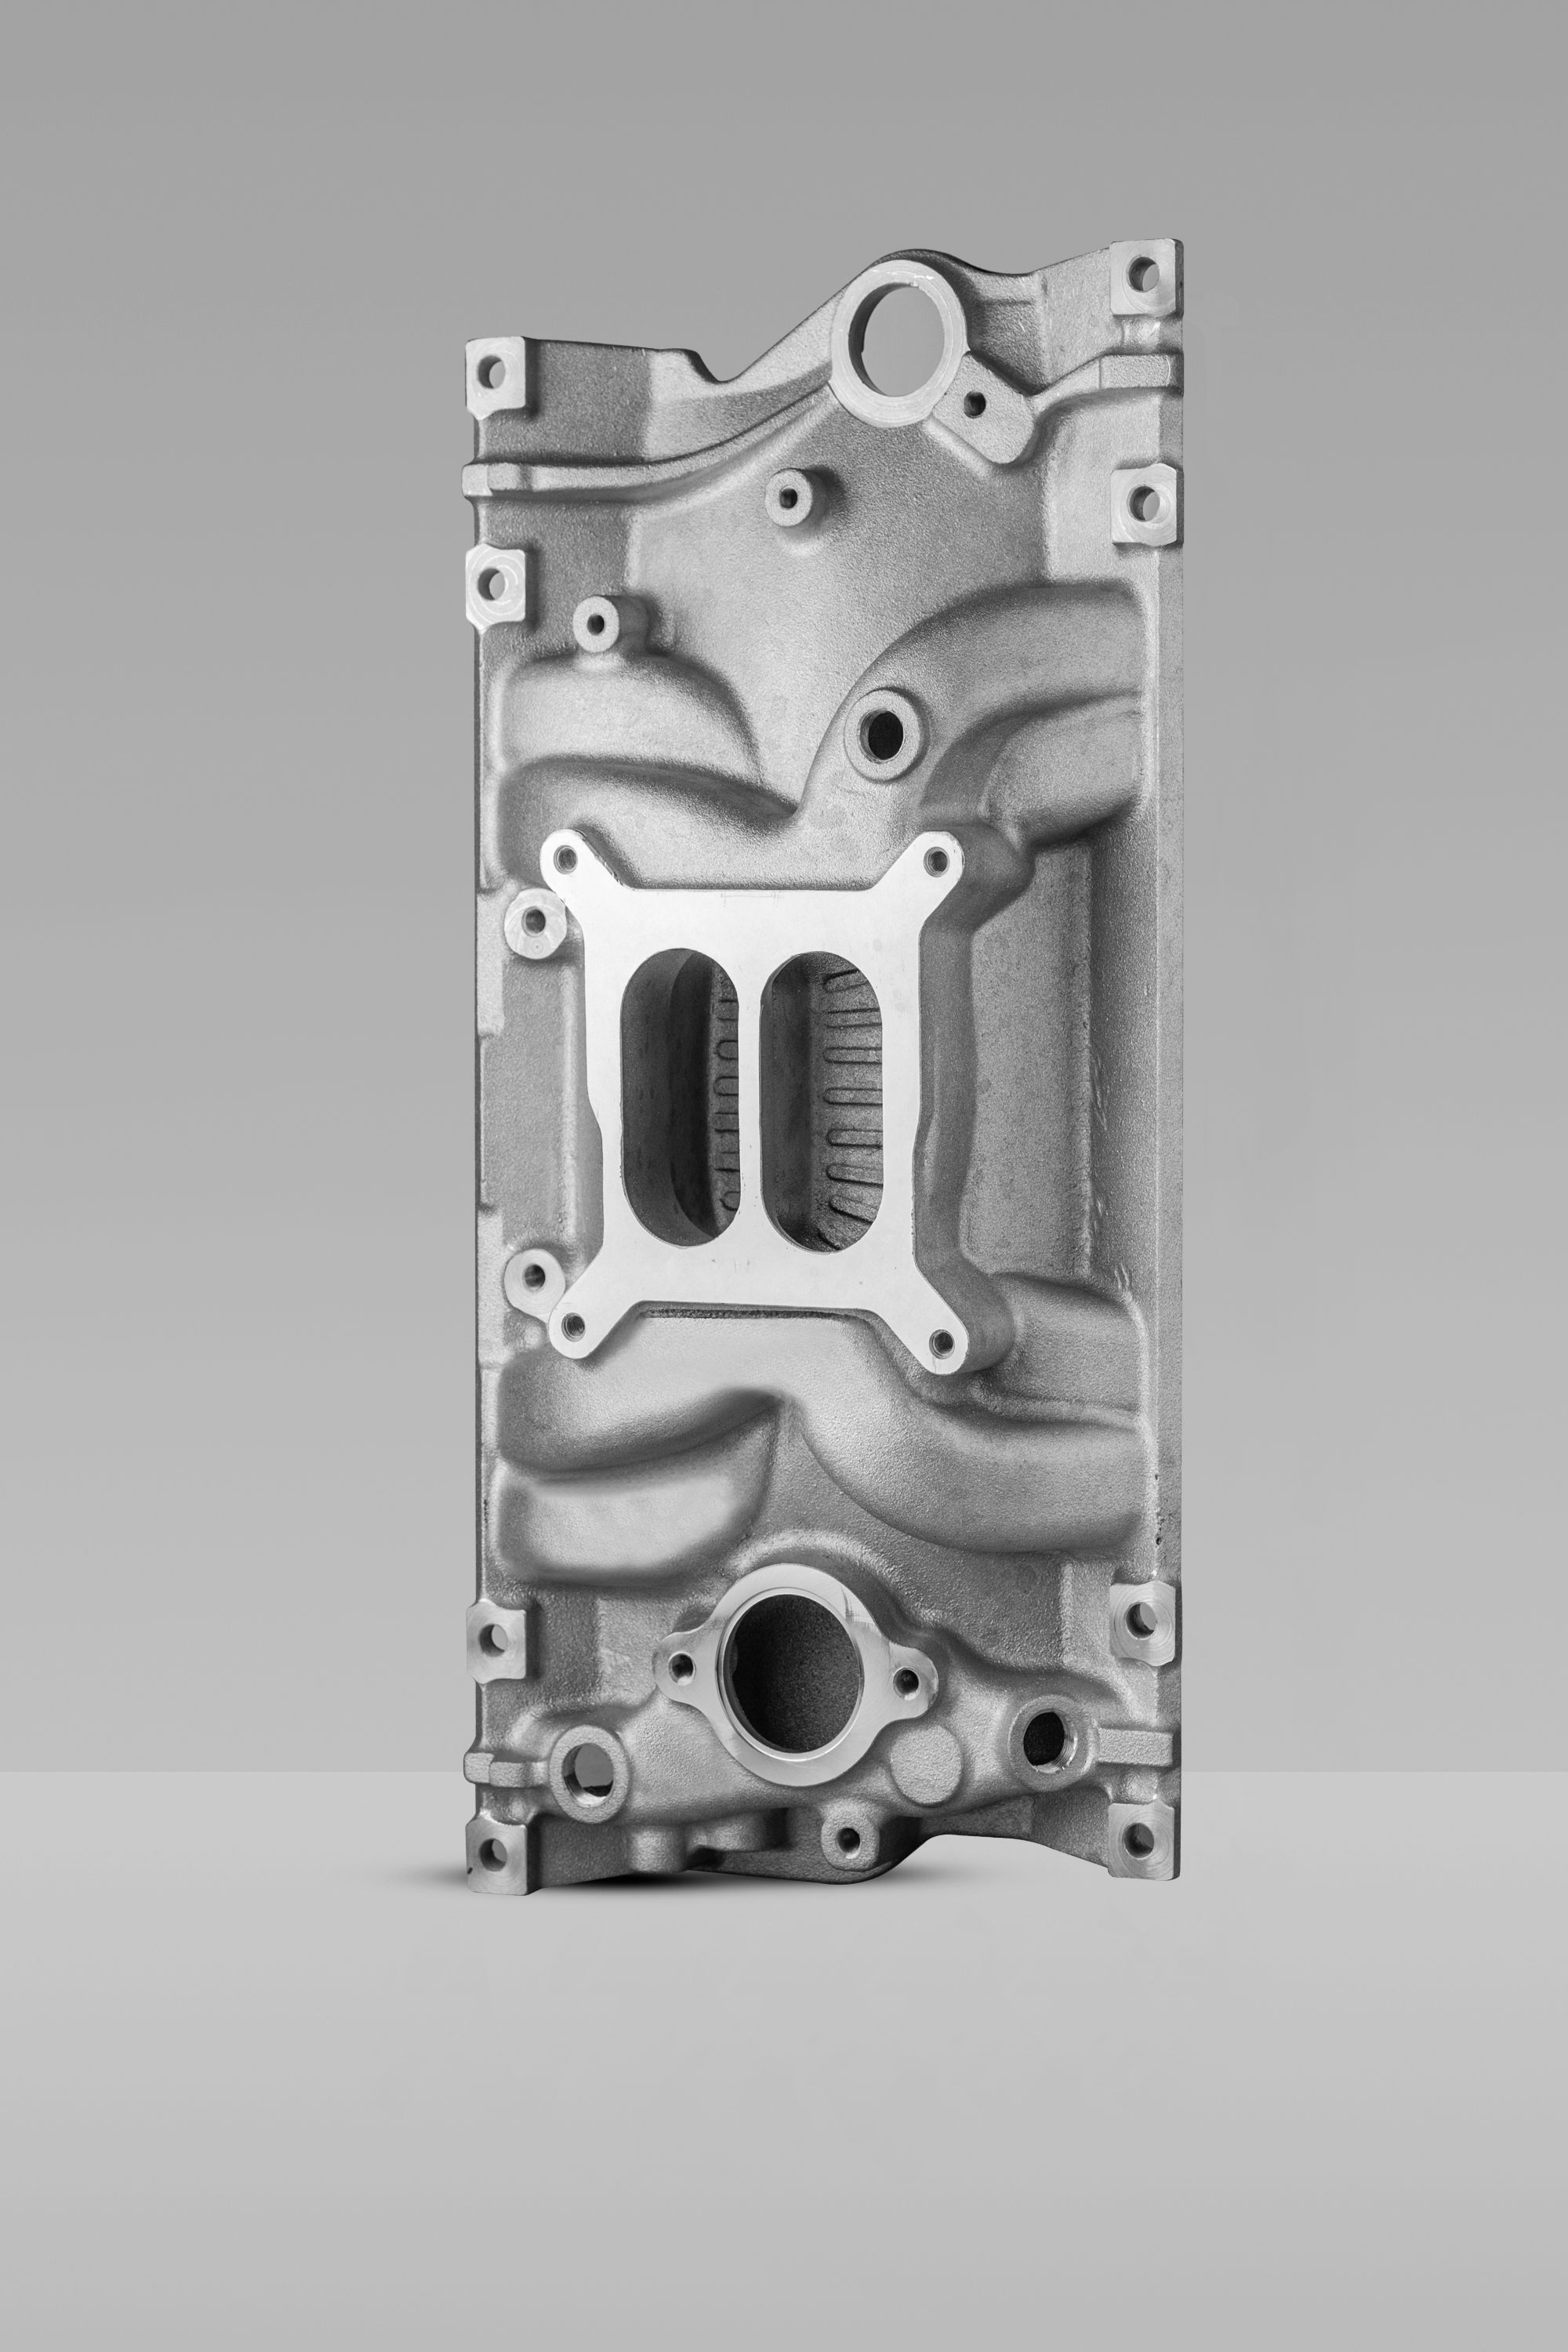
Port matching is rarely about making every surface mirror-smooth. The real gains come from eliminating abrupt steps where the intake manifold meets the cylinder head, and doing so without over-polishing the bowl area. A slight texture on the port walls actually helps keep fuel suspended in the air stream, especially on carbureted or throttle-body injected engines. So the first secret is knowing when to stop grinding—smooth the transition, not the entire port.
Another overlooked detail is the gasket itself. Even a perfectly matched port can be ruined by a gasket that protrudes into the airflow path. Trace the actual runner opening onto the gasket with a scribe, then trim it back to the line. Use the head as your template, not the manifold, because the head port is usually the smaller of the two. If you make the manifold slightly larger than the head port, you create a step that acts like a one-way valve—fine for preventing reversion, terrible for peak flow.
Finally, don't chase flow bench numbers blindly. A port that flows 10% more on the bench can still lose power if the velocity drops too much. Focus on keeping the cross-sectional area consistent from the plenum to the valve seat. Small, deliberate changes—like radiusing the short-side turn or blending the injector boss—often outperform a full porting job that enlarges everything. Flawless airflow is about balance, not just volume.
Inside Our CNC Manifold Production Line
Walking onto the floor where our CNC manifolds take shape, the first thing you notice is the steady rhythm of machines and people working in sync. Raw aluminum and stainless steel billets are loaded into five-axis machining centers, each one programmed with toolpaths refined over hundreds of runs. The coolant mist hangs faintly in the air as spindles spin at high speed, carving fluid channels and sealing faces with tolerances that stay within a few microns. Operators don't just watch screens; they run their fingers over fresh-cut surfaces, check chip formation, and make small offset adjustments on the spot.
Further down the line, every manifold passes through a dedicated inspection cell before it moves to deburring and pressure testing. Here we use coordinate measuring machines and custom fixtures that replicate real mounting conditions, so any deviation shows up early. Batch records travel with each part, noting tool wear, probe data, and final torque specs. It's not a fully automated lights-out setup—people still make the final call on surface finish and fit—but that mix of careful hands and precise machining is exactly what keeps reject rates low and delivery dates honest.
Why Wall Thickness Dictates Power Delivery
Thin insulation seems attractive until you look at what happens under sustained load. A cable’s wall thickness directly shapes how much dielectric stress the material can absorb before partial discharge begins, and once that threshold is crossed, failures accelerate quickly. More material doesn’t just add mechanical toughness—it spreads the electric field over a larger radius, lowering the volts-per-mil gradient inside the jacket. That’s why two conductors with identical copper can have wildly different voltage ratings simply because one was extruded with a thicker wall.
Heat tells a similar story. Wall thickness determines the thermal resistance between the conductor and ambient air, and every extra fraction of a millimeter changes how fast a cable sheds the heat generated by I²R losses. If the wall is too thin for the load profile, the insulation softens, ages faster, and eventually loses its dielectric strength. On the flip side, an overbuilt wall can trap heat and reduce ampacity. The real skill lies in matching wall thickness to the operating voltage, duty cycle, and environment—because that dimension isn’t just a protective shell, it’s the factor that decides whether power gets delivered reliably or becomes a failure point.
Customer Builds: Manifolds for Unusual Engine Swaps
Every now and then a customer rolls in with an engine that was never meant to live in the chassis it's sitting in. A rotary in a Datsun, a V12 in a vintage pickup, a diesel inline-six squeezed into a sports car that originally had half the cylinders. These aren't off-the-shelf projects, and nobody makes a manifold for them. That's where the fun starts.
We look at the existing ports, the physical clearance around the headers, and the owner's driving habits. Sometimes the goal is torque off idle for a street cruiser; other times it's all top-end flow for a track toy. From there we sketch, prototype, and tweak until the runners match the engine's character rather than just bolting up. Weld placement matters more than people expect—a tight merge collector can wake up a lazy low end, while longer primaries stretch the powerband on a high-revving swap.
The best part is seeing a manifold come back from a track day with discoloration right where we predicted the heat would concentrate. It means the flow is doing the work, not fighting the plumbing. And when someone asks the owner where they bought the headers, the usual answer is a shrug and a nod toward our shop.
Heat Management Tactics for High-Boost Applications
When boost levels climb, intake air temperatures can spike dramatically, robbing power and inviting detonation. A properly sized intercooler becomes non-negotiable. Rather than simply bolting on the largest core available, pay attention to end tank design, fin density, and airflow path. For street cars, a well-ducted air-to-air unit often outperforms a poorly placed water-to-air setup. If packaging constraints force a front-mount location, ensure the radiator and condenser are not choking flow. Ducting and sealing gaps matter as much as core volume; air will always take the path of least resistance.
Underhood heat management is equally critical. Turbo blankets and ceramic-coated exhaust manifolds keep radiant heat from baking nearby sensors, hoses, and wiring. Wrapping downpipes may draw mixed opinions, but on a high-boost engine the reduction in engine bay temperatures is measurable. Think beyond just shielding: hood vents or extractor scoops help evacuate hot air at speed and while stationary. Even small changes, like using reflective tape on intercooler piping or relocating coolant reservoirs away from the turbo, add up.
Engine oil and coolant must handle the extra thermal load. Upgraded oil coolers with thermostatic control prevent oil from thinning and losing film strength under sustained boost. A high-capacity radiator with a well-designed shroud and proper fan control can hold coolant temps stable during repeated pulls. For those chasing every degree, water-methanol injection offers direct charge cooling, though it requires careful tuning and system monitoring. The goal is not just lower peak temperatures; it is consistency lap after lap, pull after pull.
FAQ
They design and build intake manifolds from aluminum, usually to match a specific engine or power goal. That means cutting runners, shaping a plenum, welding it all together, and then machining flanges so it seals properly against the heads.
Aluminum takes heat and boost pressure better than most plastic intakes. It won’t warp or crack as easily in a high-horsepower setup, and if you need to change runner length or add a port later, a fabricator can weld and re-machine it without starting over.
Check their past work with real engine bay photos or customer builds. Ask about the alloy they use, how they keep the flange flat during welding, and whether they pressure test each manifold before it ships. A quick video of that test is a good sign.
Realistically, it depends on your whole combination—cam, heads, compression, and tune. A well-designed manifold can fatten up the midrange and sometimes add 10 to 30 horsepower over stock, but anyone promising an exact number before seeing your setup is guessing.
Yes, most experienced builders do both. Forced induction manifolds usually use shorter runners and a stronger plenum to handle pressure, while naturally aspirated pieces focus more on runner length and taper to suit your cam’s RPM band.
Make sure you pin down flange thickness, injector bung location, and the throttle body opening size. Also tell them early if you run drive-by-wire or cable throttle—some builders default to cable unless you say otherwise.
Aluminum is easy to weld and machine, so most repairs and changes are doable. If you swap heads or want bigger injector ports later, a good fabricator can often modify the existing manifold instead of building a new one.
Typical lead time is two to six weeks, depending on how many jobs are ahead of yours and how much hand work the design needs. A one-off manifold with an integrated intercooler core or unusual runner layout can take longer.
Conclusion
Not every foundry pours the same 6061, and we settled on 356-T6 for most cast runners because it welds clean and stays dimensionally stable after thermal cycling. For high-boost or one-off billets, 7075 occasionally appears, but it is too crack-prone for long runners, so we usually machine from solid 6061 instead. Port matching is where a manifold earns its keep. A mirror polish at the entry actually hurts fuel suspension, so we leave a fine crosshatch near the injector boss and blend only the last inch to the cylinder head. On the CNC line, each casting is measured at three datums before any tool path runs. Thin walls tend to deflect and sing during cutting, so the spindle speed gets dialed back on the plenum roof while the flange face is finished with a 0.010-inch step-over. That mix of probing and adaptive feed keeps scrap under two percent.
Wall thickness is not a single number on our manifolds. Runners start at 0.120 inch at the plenum, taper to 0.080 inch two inches from the head flange, and the plenum floor gets an extra 0.040 inch for high-boost builds. That taper moves the torque peak up or down by several hundred rpm, so we adjust it for each customer's cam and turbo sizing. We have cast manifolds for a supercharged inline-six dropped into a 1970s farm truck and a motorcycle-derived four-cylinder wedged into a first-gen Mini, and both required different runner lengths, thermostat relocations, and even a side-mount throttle body. Heat management in high-boost applications is mostly about keeping the plenum from heat-soaking the air. We add a 0.100-inch air gap under the floor and ceramic coat only the outside of the roof, leaving runners bare so they can shed heat into the airstream. It is a small touch, but it keeps intake air temps down without adding a bulky intercooler.
Contact Us
Contact Person: Shelly
Email: [email protected]
Tel/WhatsApp: 8613967667688
Website: https://www.yongyu.com/